Industry Standard Precision
Our services cover parts up to 12”x12”x6” with standard tolerances of +/- 0.005”, hole tapping, and standard finishing (media blasting and type II anodizing).
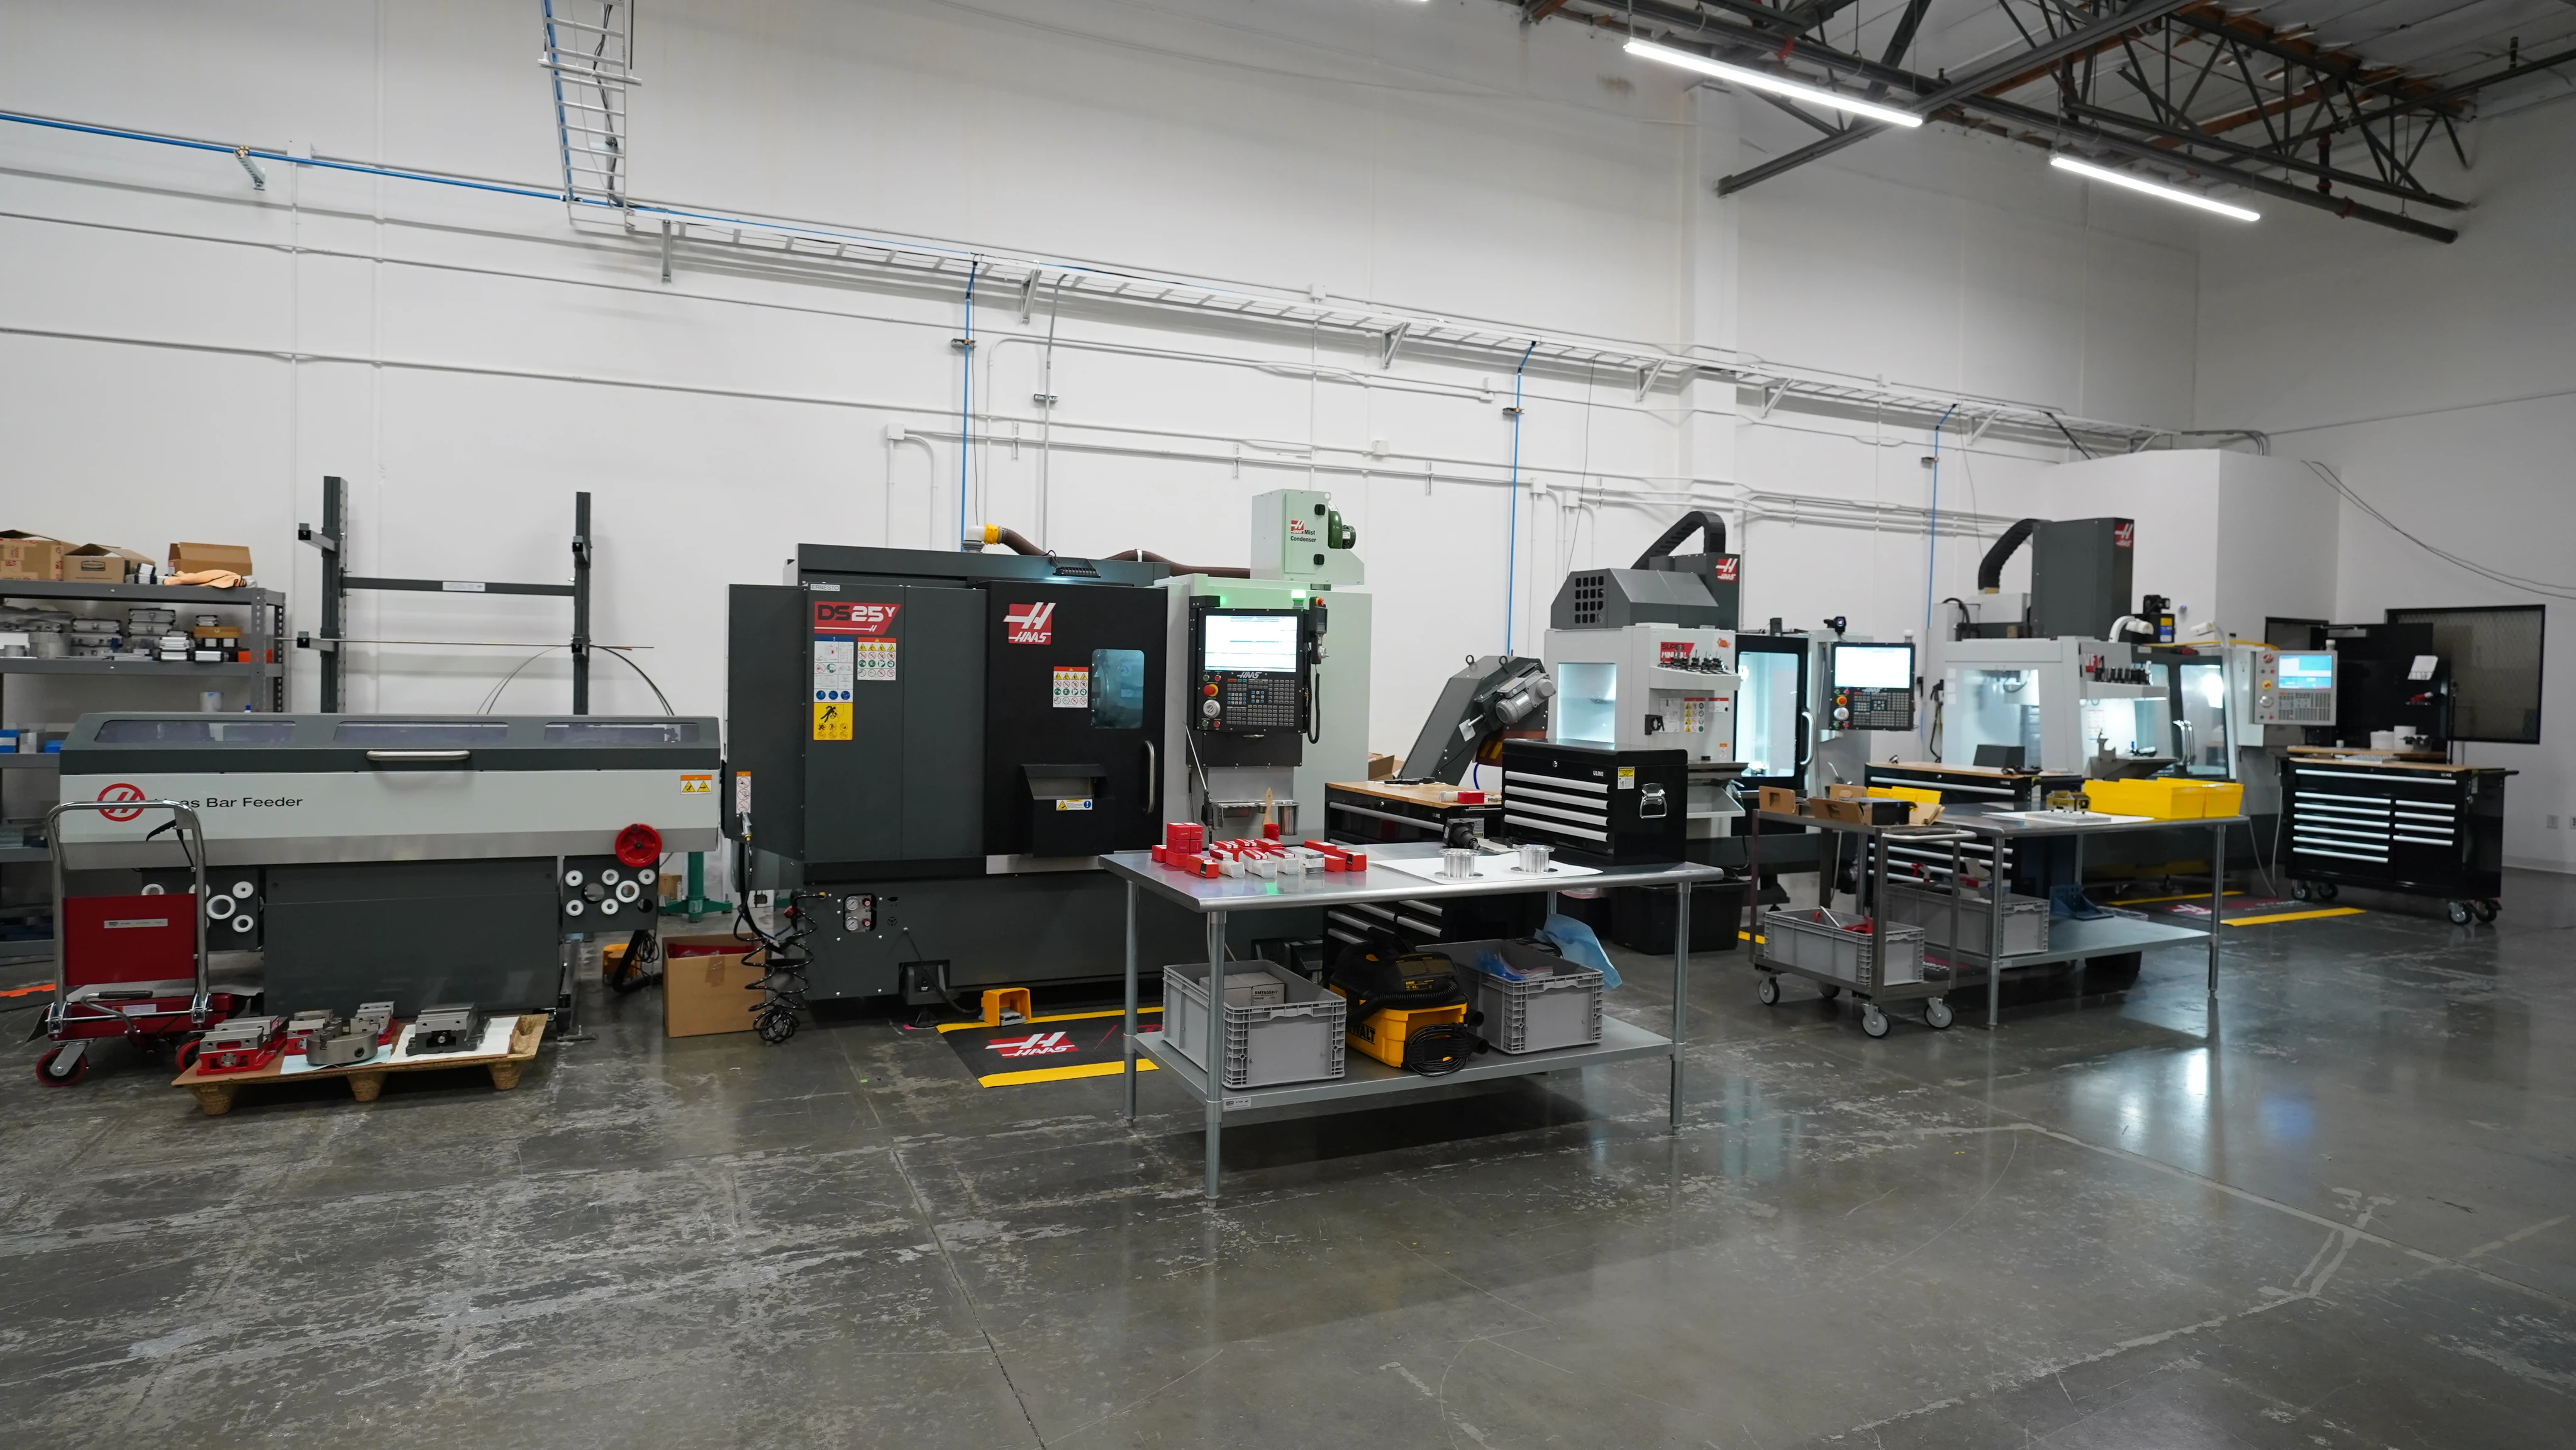
Get your parts manufactured at our machining facility and shipped to your door.
We offer 3-axis and 3+1-axis CNC machining in multiple aluminum alloys, and our capabilities are growing every day.
Now accepting customers to join our manufacturing beta - submit a part for consideration and we'll get in touch with you.
Get early access to CNC machining at Zoo. We’re welcoming select customers to make parts in our shop and share feedback that helps shape how we work. Just submit a part for approval and we’ll be in touch within 2 business days.
Choose Zoo for manufacturing →
Our services cover parts up to 12”x12”x6” with standard tolerances of +/- 0.005”, hole tapping, and standard finishing (media blasting and type II anodizing).
Our standard production time is 5-7 business days, plus standard or expedited shipping. We provide estimated production and delivery times with your quote.
Choose from multiple aluminum alloys to match your design’s demands—from versatile 6061 for everyday parts to high-strength 7050 and 7075, and fatigue-resistant 2024.
Our CNC machining shop is still in beta and we are constantly evolving. Expect expanded material options, increased capacity, and streamlined workflows as we continue to advance the seamless integration between hardware and software.
We offer quick-turn 3-axis CNC machining in aluminum for single-part designs. Parts are considered on a case-by-case basis; we may not be able to handle all parts at this time. Our services cover parts up to 12”x12”x6” with standard tolerances of +/- 0.005”, hole tapping, and standard finishing (media blasting and type II anodizing).
Before you submit
Upload one STEP or KCL model containing the individual part you’d like manufactured.
For threaded holes, you can attach one PDF identifying the thread specifications and locations. Its dimensions must agree with the model.
Check that your part fits within our 12”x12”x6” work space. Deep features may limit acceptance.
Allow for rounded internal corners. Our minimum corner radius is 1/16”. Pocket depth must not exceed 2”.
Use drilled holes at least 1/16” (1.587 mm) in diameter with depths not greater than five times the diameter.
Ensure cutting tools can reach the features. Inaccessible overhangs and enclosed voids cannot be machined.